Email: [email protected]
Email: [email protected]
Industry News
 Home / News / Industry News / Portable Spot Welder Factory: The Machine That Joins Sheet Metal in Half a Second
 2026.10.16
 Industry News
Two pieces of sheet metal overlap. The electrodes clamp down. The current surges through the contact point, the resistance generates the heat, and the metal fuses. The whole cycle takes less than a second. A portable spot welder factory builds the machines that do this on the auto body panel, the HVAC duct, and the sheet metal bench. The welder is not a MIG and not a TIG. It is the resistance welder, and it does one job very fast.
The spot welder is built around a transformer. It steps the line voltage down to a few volts and the current up to thousands of amps. The low voltage and the high current are what make the weld. The transformer is the heaviest part of the machine, and the portable version uses a smaller core with a lower duty cycle.
A portable spot welder factory winds the transformer for the specific current and the duty cycle. The welder that runs a spot and then cools is the portable unit. The welder that runs continuously is the bench model with the water cooling.
The electrodes are copper alloy tips that contact the metal. They carry the current and apply the squeeze force. The tip diameter sets the weld nugget size. The tip wears with every weld and has to be dressed or replaced.
A portable spot welder factory supplies the electrodes and the dresser. The welder that runs a worn tip gets a weak weld. The welder with the right tip and the right dressing schedule gets the consistent nugget.
The weld cycle has three steps. The squeeze is the electrode force applied before the current. The weld is the current burst. The hold is the force maintained after the current to let the nugget cool under pressure. The timer controls all three.
A portable spot welder factory builds the timer and the air or manual squeeze system. The welder with the right squeeze, weld, and hold times produces the nugget that holds. The welder with the wrong times produces the cold weld or the burn-through.
Here is what a portable spot welder factory has to deliver:
The auto body shop uses the portable spot welder to attach the panels. The welder reaches into the wheel well and the door frame. The weld has to match the factory spot welds. The sheet metal shop uses the welder for the ductwork and the enclosures. The HVAC installer uses the portable welder on the job site.
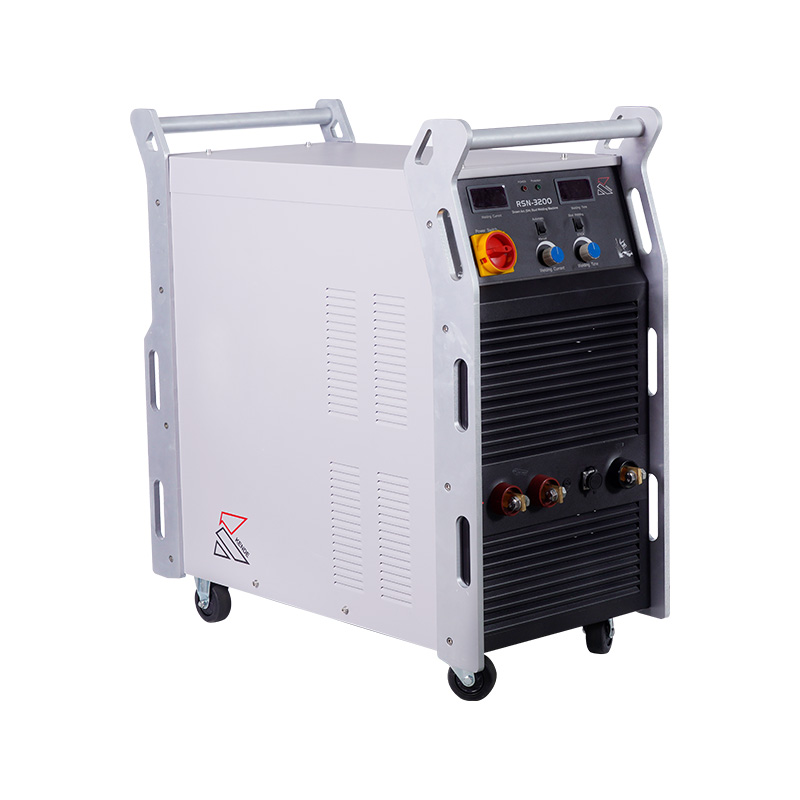
The weld does not hold because the current was too low or the time was too short. The welder with the published settings prevents the cold weld. The weld burns through because the current was too high or the squeeze was too light. The proper setting and the force prevent the burn. The electrode sticks because the tip was dirty or worn. The clean, dressed tip prevents the stick.
A portable spot welder factory builds the machine that joins the sheet metal in half a second. The transformer delivers the current. The electrodes deliver the squeeze. The timer delivers the control. Choose a factory that builds the consistent output and supplies the electrodes and the charts.
Recommended Products
Contact Us
No.2299, Luqiao Section, Shugang Avenue, Luqiao District, Taizhou, 318057 Zhejiang, PR China.
+86-576-82431568
 Privacy
China Welding Machine Factory
 English
 中文简体
 русский
 Español
 عربى
 Français
 Português
 Deutsch
 Український