Email: [email protected]
Email: [email protected]
Industry News
 Home / News / Industry News / Portable Spot Welder Factory: The Machine That Joins Sheet Metal in a Flash
 2026.09.25
 Industry News
A spot welder joins two pieces of sheet metal by passing a large current through them at a single point. The resistance at the contact point generates the heat, and the metal fuses. No filler rod. No shielding gas. Just two electrodes squeezed together and a burst of current. A portable spot welder factory builds these machines small enough to carry to the job: the auto body shop, the HVAC install, the sheet metal shop. The weld happens in a fraction of a second, and the machine has to deliver the same current every time.
The spot welder is a transformer machine. The transformer steps the voltage down and the current up. The low voltage, often just a few volts, and the high current, often thousands of amps, are what make the weld.
A portable spot welder factory winds the transformer for the specific current and duty cycle. The transformer is the heaviest part of the machine. The portable version uses a smaller core and accepts a lower duty cycle. It welds a spot, then cools before the next one.
The current has to be consistent. A weld that gets less current than it needs is a cold weld that holds nothing. A weld that gets too much burns through the sheet. A portable spot welder factory that controls the transformer output and the timing produces the consistent weld.
The electrodes are copper alloy tips that contact the metal. They carry the current and apply the pressure. The electrode shape and the tip diameter determine the weld nugget size. A portable spot welder factory that supplies the right electrode for the material and the thickness produces the weld that holds.
The squeeze is the force the electrodes apply to the metal. The force has to be enough to make good contact and contain the weld. Too little and the metal arcs and the weld is poor. Too much and the electrodes indent the surface.
The electrode tips wear. The copper erodes and the tip flattens. A portable spot welder factory that makes the tips replaceable and supplies the replacement keeps the machine welding.
The weld time is measured in cycles, fractions of a second. The timer controls how long the current flows. The right time depends on the material, the thickness, and the current. A portable spot welder factory that provides the weld time chart for the common materials gives the operator a starting point.
The control also handles the squeeze time and the hold time. The squeeze happens before the current, the hold happens after. A portable spot welder factory that sequences the three steps correctly produces the weld that forms and cools under pressure.
Here is what a portable spot welder factory needs to deliver:
The auto body shop uses the portable spot welder to attach the panels. The machine reaches into the wheel well and the door frame. The weld has to match the factory spot welds. A portable spot welder factory that supplies the body shop with the right electrodes and the right settings serves the trade.
The sheet metal shop uses the spot welder for the ductwork and the enclosures. The machine sits on the bench or hangs from the balancer. The welds are fast and clean.
The HVAC installer uses the portable welder on the job site. The machine runs on the available power. The weld has to hold the duct.
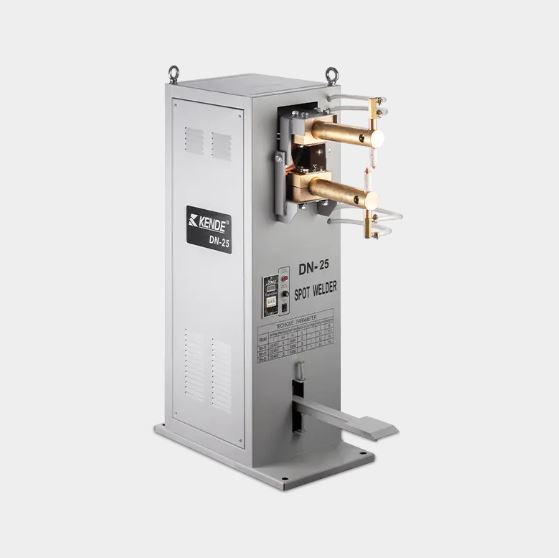
The weld does not hold because the current was too low or the time was too short. A portable spot welder factory that publishes the settings prevents the cold weld. The weld burns through because the current was too high or the squeeze was too light. The proper setting and the proper force prevent the burn. The electrode sticks because the tip was dirty or worn. The clean, dressed tip prevents the stick.
A portable spot welder factory builds the machine that joins sheet metal in a flash. The transformer delivers the current. The electrodes deliver the squeeze. The timer delivers the control. Choose a factory that builds the consistent output and supplies the electrodes and the charts. The weld will hold and the panel will stay.
Recommended Products
Contact Us
No.2299, Luqiao Section, Shugang Avenue, Luqiao District, Taizhou, 318057 Zhejiang, PR China.
+86-576-82431568
 Privacy
China Welding Machine Factory
 English
 中文简体
 русский
 Español
 عربى
 Français
 Português
 Deutsch
 Український